A wholesale toothpaste range rarely needs many pack sizes, but the ones you keep have to do different jobs. Choose each size from three inputs: its shelf role, the declared net content it carries, and the cost it adds per 100 g once packaging is counted. Confirm fill weight and tolerance against the current batch record before accepting a quotation.
1. Give each size a job before you give it a number
Three roles cover most ranges. Write the role down first; the gram figure follows from it.
| Role | What it must do | What to confirm before approving |
|---|---|---|
| Entry or trial size | Lets a retailer test the range | Declared net content and unit, target fill weight, and whether the tube is a shorter core tube |
| Core repeat size | Carries the volume in the second and third order | Units per carton, cartons per layer and pallet build, on the current pack revision |
| Family or value size | Higher spend per pack | Packed carton weight against the receiving limit, and whether the receiver de-stacks by hand |
Each row is a separate SKU, not a variant: its own artwork, net content declaration, barcode and usually its own minimum run. A range of five sizes is five of each.
2. Three numbers that are not the same number
Buyers say "the 100 g tube" and mean three different figures. A supplier answering a different one is not being evasive.
- Declared net content is the quantity printed on the pack, in the unit the destination market requires.
- Target fill weight is the production set point, which may sit above the declared figure.
- Fill tolerance is the accepted range either side of that target, and the reason two packs of one SKU can differ.
Ask which figure appears on the artwork, which on the batch record, and how the line checks it: by weight or by volume, and what the checkweigher logs. Confirm the tolerance against the current batch record, not a specification written for another run.
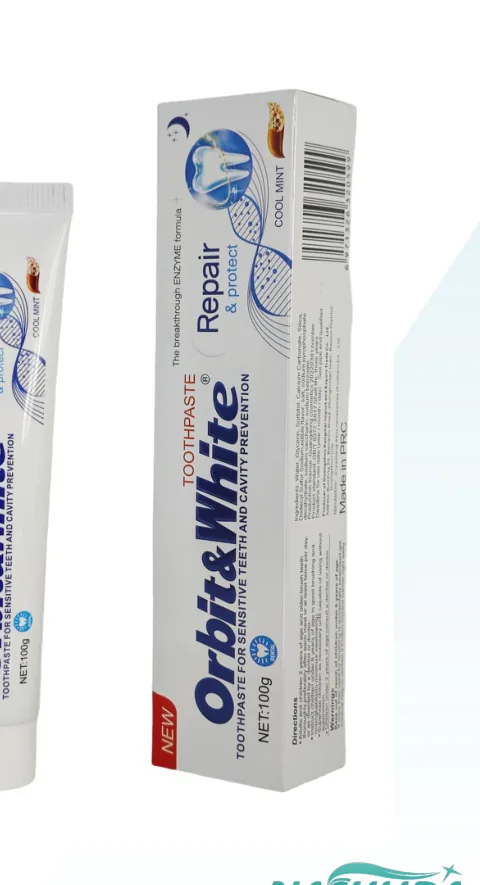
Fit is a separate question. A tube must hold the fill plus headspace for sealing, so a pack that reads as half empty is a component-fit problem, not a filling error.
3. Millilitres and grams are not interchangeable
Paste density varies with the formula, so a volume declaration is not a weight declaration: a 100 ml bottle and a 100 g tube are not equal quantities. Where a line in our bottled range is declared by volume, ask for the density figure used for any conversion, and confirm the required unit with your importer of record. The declaration rule belongs to the market the goods are sold in, not the factory that filled them.
4. Compare sizes on cost per 100 g, not on unit cost
Divide the all-in cost of one finished pack by its net content in 100 g units: the only figure that compares sizes fairly, because packaging does not shrink with fill. Every number below is an assumption chosen to show the arithmetic, not a quotation.
| Figure, assumed | 50 g entry | 100 g core | 150 g family |
|---|---|---|---|
| Paste, indexed to fill | 50 | 100 | 150 |
| Pack components, indexed | 55 | 60 | 68 |
| Finished pack, indexed | 105 | 160 | 218 |
| Cost per 100 g, indexed | 210 | 160 | 145 |
The last row carries the point: the entry size sits 50 index points above the core size per 100 g, because tube, cap and carton are paid for once regardless of what goes inside. That is not a reason to drop the small size, but it is a reason to state what the small size is for.
Order-level costs move the same way. Artwork, plates, sampling and freight are paid per order, so a trial split across four sizes spreads them over fewer units: fewer sizes, deeper, costs less per unit at the same volume. That is the allocation question the SKU assortment worksheet sets out.
5. How many sizes a trial order can carry
Size count should follow the volume you can commit per SKU, not the shelf you would like to occupy. Two tests keep the ladder honest.
- Run-size test. Can each size take the minimum run without leaving stock the buyer cannot sell? If not, that size waits.
- Case test. Does each size produce a carton and pallet build you can ship? Units per carton change with the pack, so re-run the carton specification and the pallet arithmetic for every size instead of assuming the core size's build carries over.
A workable sequence is two sizes for the trial, a documented reason for the third, and a review after the first reorder. Each size needs its own barcode and artwork revision, so confirm who owns the numbering. When one order carries several sizes, the mixed-SKU checklist covers the packing questions.
6. The size ladder worksheet
One row per size, filled from documents rather than memory.
| Field | What goes in it |
|---|---|
| Role | Entry, core or family, and the reason this size exists |
| Declared net content | Figure and unit, as it will appear on the pack |
| Fill and tolerance | Set point and accepted range, from the batch record |
| Pack reference | Tube diameter and length, or bottle reference, with revision |
| Case build | Units per carton, cartons per layer, layers per pallet |
| Cost index | Cost per 100 g, from your quotation lines |
| Decision | Approve, defer or drop, with the date and the evidence |
Send your destination market, the roles you need filled, the net content you intend to declare and the quotation lines you hold. We will say which figures are confirmed for the current pack revision and which still need measuring, using our NASHUDA tube range as the reference.
Send your range requirements to our team — destination market, series, sizes and quantities you are considering.